Cross-cut adhesion inspection of marine coatings
Introduction
During the maintenance of ships, partial repair of coatings is a routine operation. The bonding between the repair layer and the original coating or substrate is directly related to the long-term protection effect and durability of the repaired area. Insufficient bonding can lead to early peeling of the coating, accelerating substrate corrosion and affecting ship safety and operational cycles. Therefore, it is crucial to scientifically and accurately evaluate the adhesion of the patch layer. As an intuitive and efficient qualitative or semi-quantitative method, grid adhesion testing is widely used in the field and laboratory to test the adhesion performance of coating systems. This article discusses how to use the grid adhesion meter to standardize the bonding force of the repair layer of ship coatings.
Grid method test principle
The basic principle of grid testing is to use a specific size cutter to cut grid-like scratches perpendicular to each other on the surface of the coating until it penetrates the coating to the substrate. Subsequently, special tape is used to adhere to the mesh area and peel off quickly, and the adhesion grade is evaluated by observing the peeling of the coating in the mesh area. This method mainly evaluates the resistance to separation between the coating and the substrate, or between the layers of the coating system. Its physical process involves the cohesion of the coating, the adhesion of the interface, and the stress transfer under the action of external forces. The test results are influenced by various factors such as coating thickness, flexibility, drying and curing degree, and substrate surface condition.
For quantitative evaluation, a simplified model is often introduced to understand interface binding energy. It is assumed that the peeling process mainly overcomes the binding energy of the interface, and the binding energy per unit area is WaIt can be approximated as:
Wa ≈ F / w
where F is the peel force and w is the peel width. In the actual grid test, the peeling force F of the tape is relatively constant, so the area ratio of coating peeling intuitively reflects the binding energy of the interface WaThe relative strength of the The smaller the peeling area, the stronger the binding force.
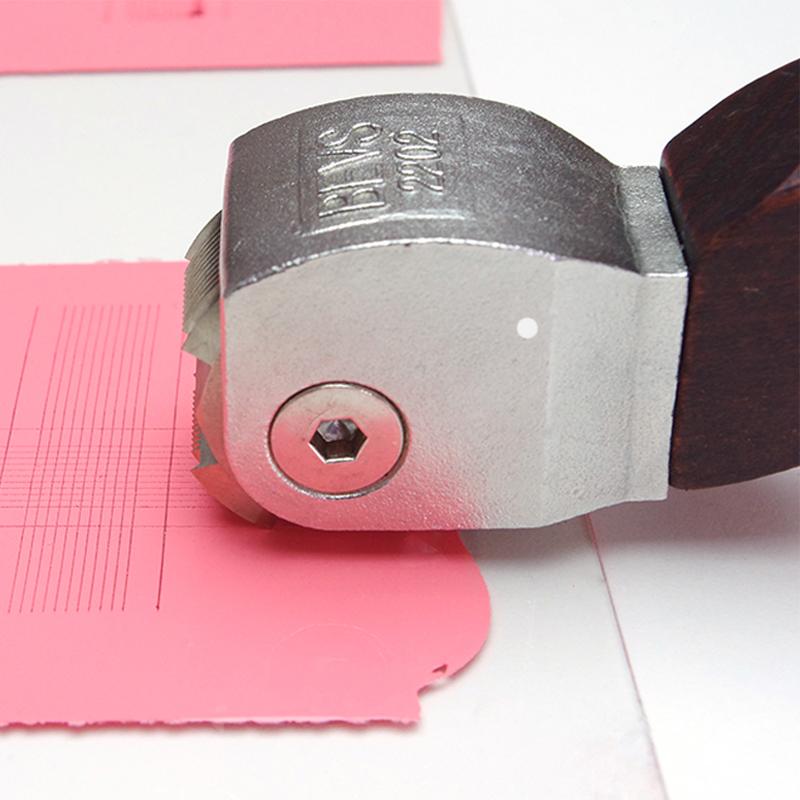
Test Instruments & Tools
Standard grid testing requires a sophisticated set of tools to ensure reproducibility and comparability of results. The core instrument is the gridr, and its key component is the multi-edge cutting tool. The cutting edge spacing of the tool determines the size of the grid, and the common specifications are 1 mm, 2 mm, etc., which need to be selected according to the relevant standards according to the total thickness of the coating. In addition, the kit often includes a soft-bristled brush, magnifying glass, lights, and pressure-sensitive tape that meets the requirements of the standard. The adhesion strength of the tape must be stable, and its peel strength is usually specified in the standard, for example, it is required to be (10 ± 1) N/25mm. All tools should be kept clean before and after use, and the cutting edge must be sharp, as dull edges can cause coating crushing instead of clean cuts, affecting test accuracy.
| Tool Name | Main functions and requirements |
| Multi-blade gridr | Perform parallel cutting with precise spacing, and the edge spacing error should be less than 5%. |
| Standard pressure sensitive tape | Provides stable, uniform adhesion for peeling loose coatings from gridded areas. |
| Observe the magnifying glass | Typically 2x to 5x magnification for clear assessment of mesh peeling. |
| Soft bristle brush | Gently brush the coating chips from the cut diagonally to avoid artificial peeling. |
Test process and operation points
Testing marine coating repair layers requires strict steps. First, select a representative patching area, the surface should be clean, dry and flat. The temperature and humidity of the test environment should meet the requirements of the coating product manual or relevant test standards, and it is generally recommended to carry out under the conditions of (23±2)°C and relative humidity (50±5)%.
To operate, apply even and appropriate pressure with the scriber perpendicular to the coating surface to cut at a smooth speed, ensuring that all scratches penetrate the patch layer to the bottom layer. Repeat this process in directions perpendicular to each other to form a grid. When finished, gently sweep away debris diagonally with a soft-bristled brush. Subsequently, the standard tape is snugly attached to the grid area, smoothing it with your fingers or eraser to ensure no air bubbles and adequate contact. After waiting 60 to 120 seconds, quickly peel off the tape at an angle close to 180°. Finally, use a magnifying glass to carefully observe the grid area in sufficient light to assess coating peeling.
According to the particularity of the ship repair scenario, it should be noted during operation that the transition area between the edge of the repair layer and the old coating is the focus of the test; If the substrate is steel, ensure that the cutting depth is sufficient but avoid excessive damage to the substrate; In high humidity or low temperatures, the flexibility of the coating can change, which can affect test results, and environmental conditions need to be documented.
Result evaluation and grade determination
The evaluation is based on the percentage of peeling area of the coating in the grid area. The internationally accepted evaluation criteria are usually divided into 0 to 5 grades, of which grade 0 represents that the cutting edge is completely smooth and no grid falls off, indicating the best bonding force; Grade 5 represents a peeling area greater than 65%, and the worst bonding force. For ship repair layers, Grade 1 (peeling area less than 5%) or Grade 0 is usually required to ensure adequate long-term adhesion.
When evaluating, it is necessary to distinguish whether the peeling coating is the repair layer itself (cohesive failure) or the interface between the repair layer and the old coating (adhesion failure). Interface failure can directly illustrate the problem of the bonding force of the repair layer. Record of results should include test location, coating system description, grid size, environmental conditions, evaluation grade, and type of failure (cohesion or attachment).
| grade | Description (peeling condition of the cutting area) |
| 0 | The cutting edges are completely smooth and not a single frame falls off. |
| 1 | There is a slight peeling of the coating at the cutting intersection, and the affected area is less than 5%. |
| 2 | The coating peels off along the cut edge or at the intersection, and the affected area is 5% to 15%. |
| 3 | The coating partially or completely peels off a large area along the cut edge, affecting 15% to 35% of the affected area. |
| 4 | The coating peels off a large area along the cut edge, and some of the mesh peels off in its entirety, affecting 35% to 65% of the affected area. |
| 5 | The peeling area is more than 65%. |
Influencing factors and limitations analysis
The results of the grid test are affected by multiple factors. Coating factors include thickness (too thick can lead to brittle peeling), degree of curing (low cohesion if not fully cured), flexibility, and the cleanliness and roughness of the old coating surface. The rigidity of the substrate can also affect test performance. Operational factors such as cutting speed, pressure, knife sharpness, and tape application and peeling methods need to be strictly standardized.
The method also has limitations. It is primarily a qualitative or semi-quantitative method that struggles to provide precise adhesion values. For very soft or elastic coatings, assessment can be difficult. In addition, it evaluates the shear peel resistance of the coating system and may differ from other stresses (e.g., tensile, cyclic stress) that the coating is subjected to in a real-world service environment. Therefore, grid testing is often used as a tool for rapid screening and on-site quality control, and can be combined with other testing methods such as pull-open method if more accurate quantitative data is required.
Conclusion
Grid adhesion testing provides an intuitive, fast, and standardized means to evaluate the adhesion of marine coating repair layers. By standardizing the use of grids and auxiliary tools, strictly implementing the operation process, and conducting objective evaluation according to the standard level, the quality of the repair construction and the interface reliability of the coating system can be effectively judged. Incorporating this inspection into the quality control process of the ship repair process helps to detect attachment defects in time and guide the improvement of the construction process, thereby improving the durability of the coating in the repaired area and providing support for the long-term protection of the ship structure. In practical application, the applicable conditions and influencing factors of the method should be fully understood, and if necessary, it should be combined with other test methods for comprehensive judgment.
References
ISO 2409:2020, Paints and varnishes — Cross-cut test.
ASTM D3359-22, Standard Test Methods for Rating Adhesion by Tape Test.
GB/T 9286-2021, Colored paints and varnishes - Grid test.
NACE SP0308-2022, Field Methods for Inspection of Coating Adhesion on Steel Substrates.
Marine and Marine Engineering Coatings and Coatings, Related Chapters, Chemical Industry Press.



- 1Cross-cut adhesion test of silicon carbon coatings
- 2Drawing method test principle [with schematic diagram]
- 3Adhesion Determination Method - Drawing Method
- 4The most complete grid measurement Adhesion: instrument selection, measurement method video and result identification
- 5Appreciation of a set of beautiful pictures of TQC CC1000 scribe
- 6Cross grid test operation video
- 7How does Adhesion evaluate?
- 8Adhesion performance test of passivating film for galvanized sheet
- 9Precautions for using the adhesion instrument