Cupping test machine to evaluate deformation resistance of automotive steel coatings
Introduction
In automotive manufacturing, the integrity of surface coatings is crucial for the long-term durability and appearance of products. Coatings need to withstand stamping, assembly, and mechanical deformation in everyday use without cracking or peeling. Therefore, the scientific evaluation of the deformation resistance of the coating substrate composite system has become a key link in the quality control of materials and processes. As a classic mechanical property testing method, cupping test provides a reliable basis for quantitatively evaluating the bonding properties and ductility of coatings and substrates (such as automotive steel plates) by simulating the deformation process of materials under bidirectional tensile stress. This article will systematically explain how to use a cupping testing machine to evaluate the deformation resistance of automotive steel plate coatings, covering the test principle, standard method, key parameters and result analysis.
Test principle
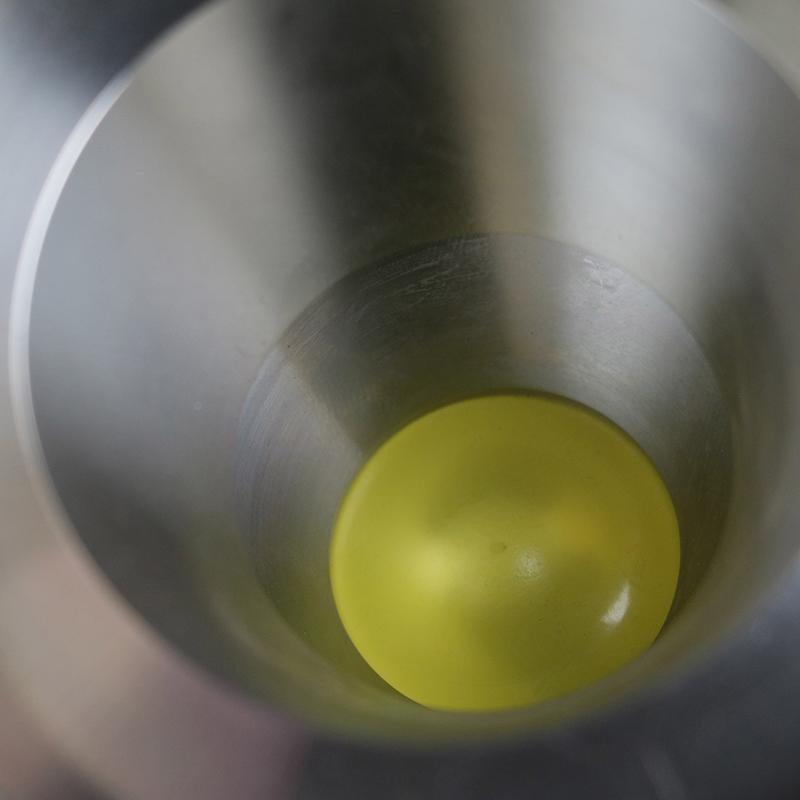
The basic principle of the cupping test, also known as the Erickson cupping test, is to place the clamped specimen between the die and the pressing ring, and use a spherical punch of a specified diameter to apply force to the specimen at a uniform speed, causing it to expand into the die until the coating fails for the first time (usually visible cracks or peels). At this point, the punch's depth of press, known as cupping depth, is recorded as a key indicator. This process subjected the central area of the specimen to bidirectional tensile stress, simulating the stress state of the material in forming processes such as deep drawing. For the coating system, this test effectively reflects the ability of the coating to deform with the substrate without breaking.
The critical depth (IE) of coating failure can be preliminarily theoretically analyzed by the following relationship, which correlates the basic deformation characteristics of the material:
IE ∝ (σs / E) × t
Among them, σsIt represents the yield strength of the substrate, E represents the elastic modulus of the coating material, and t is the thickness of the coating. This formula shows that the cupping depth is correlated with the strength of the substrate, the flexibility and thickness of the coating. However, the actual performance is the result of the synergy between coating adhesion, cohesion, ductility and substrate properties.
Test equipment and standards
The standard cupping and burst testing machine is mainly composed of a frame, a punch drive system, a clamping device (pressing edge and die), a measuring system (the depth measurement accuracy is usually required to be 0.05mm) and a specimen clamping force control system. The diameter of the punch ball head, the diameter of the die and the clamping force should be strictly set according to relevant standards.
There are a number of standards applicable to coating evaluation at home and abroad, which need to be clearly followed during testing:
| Standard system | Standard Numbering and Names (Example) |
| International standards | ISO 1520: Colored paints and varnishes - cupping test |
| Chinese national standards | GB/T 9753: Colored paints and varnishes - cupping tests |
| Industry Applications | Often refer to the enterprise standards of automobile manufacturers |
When selecting standards, it is necessary to pay attention to their specific regulations on specimen size, pretreatment conditions, test speed (usually 0.1-0.3 mm/s), and ambient temperature and humidity to ensure the comparability of results.
Sample preparation and test steps
Specimens are typically automotive steel plates coated with a target coating and must meet standard requirements (e.g., 70 mm× 70 mm). The surface treatment of the substrate, the coating construction process and the curing conditions should be consistent with the actual production. Before the test, the specimen should be conditioned in a standard temperature and humidity environment for at least 16 hours.
The main test steps are as follows:
The specimen coating is placed facing the punch direction and firmly clamped between the pressing ring and the die.
Start the device so that the ball punch applies thrust to the center of the specimen at a constant speed.
Closely observe the coating surface of the specimen, usually from the side or front with the help of lighting.
Stop testing immediately when the coating cracks for the first time or peels off the substrate.
The pressing depth of the punch at this time is recorded, that is, the cupping depth value of the specimen.
At least three parallel specimens are tested under the same conditions, taking the arithmetic mean as the final result.
Evaluation of results and influencing factors
The cupping depth value directly characterizes the strength of the coating's resistance to deformation. The higher the value, the better the coating follows when the substrate deforms, and the stronger the crack resistance. During evaluation, the results can be compared with the requirements of product technical specifications, or used to compare the performance of different formulations and process coatings.
The main factors that affect the results of the cupping test include:
| Categories of influencing factors | Specific |
| The coating itself | Resin flexibility, cross-linking density, pigment volume concentration, adhesion. |
| Substrate characteristics | Steel plate thickness, strength, surface roughness and cleanliness. |
| Process parameters | Coating thickness uniformity, curing degree, and interlayer matching. |
| Test conditions | Clamping force, punch speed, test temperature and humidity. |
Analyzing failure modes (e.g., radioactive cracks, annular peeling) can also help locate the cause of failure, whether it is insufficient adhesion or lack of ductility of the coating.
Applications and prospects
The cupping test is widely used in the automotive industry, not only for the evaluation of steel plate veneer coatings, but also for the evaluation of coatings on substrates such as galvanized sheets and aluminum alloy plates. It is an effective screening and monitoring tool in new material development, incoming material inspection, and process optimization. With the application of lightweight automobiles and high-strength steel plates, higher requirements are put forward for the stability of coatings under higher deformation. In the future, combined with advanced observation methods such as digital image related technology, the initiation and expansion of coating failure can be more accurately captured, and the understanding of failure mechanism can be deepened, so as to guide the development of more resilient coating systems.
Conclusion
The cupping tester provides an intuitive, quantitative, and standardized method for evaluating the deformation resistance of automotive steel coatings. By accurately measuring the cupping depth of the coating at the first failure, it can effectively reflect the synergy between the coating and the substrate under complex stresses. Strict adherence to standard procedures, control of test variables, and meticulous analysis of failure modes can make this method a powerful tool to ensure and improve the quality and reliability of automotive coatings. In practical applications, the interaction between materials, processes and test conditions needs to be comprehensively considered to make accurate performance judgments.
References
ISO 1520, Paints and varnishes — Cupping test
GB/T 9753, Paints and varnishes — Cupping test
Wicks, Z. W., et al. Organic Coatings: Science and Technology.
Society of Automotive Engineers. Automotive Painting Technology.
A compilation of annual academic papers related to "Material Protection"
-
![JINGKELIAN QBJ coating Cupping test machine, paint film cupping instrument ISO1520 GB/T9753]()
-
![YONGLIDA YLD-6810 Digital Cupping test machine]()
-
![PUSHEN TQC Manual Cupping Tester Laboratory cupping testing device]()
-
![China QBJ coating Cupping tester]() China QBJ coating Cupping tester$ 820.00
-
![JFL QBJ coating Cupping tester]() JFL QBJ coating Cupping tester$ 1034.00
-
![Cupping test machine, TQC SP4400 digital display manual cupping machine]()


- 1Cupping test machine for water-based paint film flexibility
- 2Water-based paint film test, Cupping test machine is more practical to choose manual or electric
- 3Cupping test for measurement of ductility of Water-based ink coatings
- 4Cupping test of plastic coatings and films Impact ductility
- 5Cupping test machine testing metal coil coating processing forming performance
- 6Failure analysis of galvanized sheet stamping by cupping testing machine
陈思琪,王雷刚,黄瑶 - 《《基于杯突试验的镀锌板冲压成形失效分析》》
- 7Paint film flexibility bending test, which of these 5 instruments is more suitable?
- 8Cupping Testing Machine Test Coating Cupping Test
- 9Operation method and precautions of cupping instrument