Cupping test machine testing metal coil coating processing forming performance
Introduction
In the production and application of metal coils, coatings not only provide decorative and protective functions, but also their synergistic deformation ability with the substrate during subsequent processing is crucial. If the coating cracks, peels off or loses its protective properties during the molding process, it will directly affect the quality and longevity of the final product. Therefore, it is crucial to scientifically evaluate the bonding properties and durability of coatings and metal substrates during the molding process. As a classic simulated formability test method, the cupping test can effectively evaluate the processing and forming performance of metal coil coatings under complex stress conditions by using a cupping testing machine, and provide a reliable basis for material selection, process optimization and quality control.
Test principle
The core principle of the cupping test, also known as the Erickson test, is to simulate the bidirectional tensile state of the sheet metal during the stamping process. During the test, the coated metal specimen is fixed between the pressing ring and the die, and pressure is applied to the specimen through a spherical punch of a specified diameter at a constant speed to expand into the die until the coating appears to crack or separate from the substrate for the first time. The depth of the punch pressed in, known as the cupping depth, is a key indicator of the material's forming performance. The larger the depth value, the stronger the ability of the coating-substrate composite system to resist cracking during the forming process, and the better the processing and molding performance.
The stress-strain states involved in this process are complex and can be roughly described by material mechanics formulas. When a spherical punch acts on a plate, the central area of the plate is subjected to bidirectional tensile stress, and its maximum principal strain ε can be approximately expressed as:
ε ≈ ln(d/D₀)
where d is the instantaneous diameter after expansion, and D₀ is the effective diameter of the initial clamping area of the specimen. This formula simplifies how intense the sheet deforms to its condition.
Test equipment and processes
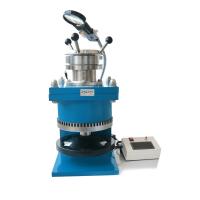
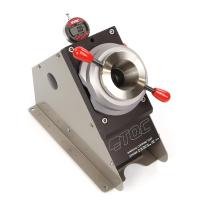
The standard cupping tester is mainly composed of a frame, a precision spherical punch, a die, an edge pressing device and a measurement control system. The dimensions of key components must strictly follow the relevant standards. The typical test process is as follows: First, a flat specimen is cut from the metal coil according to the standard. The specimen coating is then placed on the die facing the punch (or as specified by the standard), and a uniform clamping force is applied through the crimping ring to prevent wrinkling of the edges. Start the device and the punch is pressed against the specimen at a constant speed (usually 5-10 mm/min) to cause it to expand into a "cup". During the test, the failure point of the coating can be monitored by visual observation, optical magnification equipment or changes in conductivity. Record the punch displacement when the coating first cracks or peels off, i.e. cupping depth (IE value). Multiple specimens are usually tested under the same conditions to obtain an average value.

Performance evaluation indicators
The measurement of cupping depth is the most direct quantitative indicator for evaluating the processing and forming performance of coatings. However, a comprehensive assessment is not limited to this. It needs to be analyzed in combination with microscopic observation of failure modes. Common coating failure modes mainly include:
| Failure mode type | Typical characteristics and causes |
| Coating microcracks | Mesh or linear fine lines appear on the surface of the coating, usually due to insufficient ductility of the coating or excessive internal stress. |
| Coating macroscopic cracking | Obvious penetrating cracks occurred, mostly in the area with the greatest deformation, indicating insufficient fracture toughness of the coating. |
| The coating peels off | The interface separation between the coating and the metal substrate is mainly related to the adhesion and interfacial bonding strength of the coating. |
Combined with cupping depth and failure mode, a comprehensive judgment can be made on the flexibility and adhesion of the coating and the forming limit of the overall composite system. For example, a higher cupping depth is accompanied by uniform microcracks, which may indicate that the coating has good deformation following. Peeling at lower depths may indicate that interface bonding is a weak link.
Analysis of influencing factors
The cupping test results of coating-substrate composite system are affected by multiple factors, which can be mainly divided into two categories: material factors and process factors.
| Categories of influencing factors | Specific |
| The properties of the coating itself | The glass-change temperature, modulus, ductility, internal stress and thickness of the coating. In general, coatings with high ductility, low modulus, and moderate thickness perform better. |
| Substrate properties | The strength, ductility, surface roughness and pretreatment quality of the metal substrate. The formability of the substrate forms the basis of the overall performance. |
| Interfacial bonding strength | The chemical bonding and mechanical interlocking forces between the coating and the substrate directly determine the anti-peeling ability. |
| Test parameters | punch speed, edge pressing force, lubrication conditions, etc. Standardized parameters are a prerequisite for comparability of results. |
Standards & Applications
The cupping test method has been incorporated into many national and international standard systems, such as ISO 1520, ASTM E643, etc., which have made unified regulations on specimen size, equipment specifications, test speed and result evaluation, ensuring the consistency and comparability of test results. This method is widely used in fields where subsequent deformation processing of coated metals is required, such as color-coated steel plates for construction, shell plates for household appliances, metal materials for packaging containers, and pre-coated metal sheets for non-structural parts in automobiles. Through the cupping test, manufacturers can screen the coating system, R&D personnel can optimize the formula and curing process, and downstream users can formulate a reasonable processing and molding process window accordingly to avoid quality defects in production.
Conclusion
The test method provided by the cupping machine is an effective and practical means to evaluate the processing and forming performance of metal coil coatings. By simulating the bidirectional tensile state in actual molding, it comprehensively reflects the anti-cracking and peeling resistance of the coating and substrate in the process of co-deformation by quantifying the cupping depth combined with the failure mode analysis. Understanding and systematically analyzing multiple influencing factors such as coating properties, substrate state, interface bonding, and process parameters has clear guiding significance for improving the molding and processing quality and extending the service life of coated metal products. As materials technology advances, cupping testing will continue to serve as an important bridge between connection coating development, quality inspection, and molding applications.
References
ISO 1520: Paints and varnishes — Cupping test
ASTM E643: Standard Test Method for Ball Punch Deformation of Metallic Sheet Material
"Review of Formability Evaluation Methods for Coated Steel Plate Processing", Material Protection
"Research on Test Method of Forming Properties of Coating Coating of Metal Strip", Metallurgical Analysis

- 1Cupping test machine for water-based paint film flexibility
- 2Water-based paint film test, Cupping test machine is more practical to choose manual or electric
- 3Cupping test for measurement of ductility of Water-based ink coatings
- 4Cupping test of plastic coatings and films Impact ductility
- 5Cupping test machine to evaluate deformation resistance of automotive steel coatings
- 6Failure analysis of galvanized sheet stamping by cupping testing machine
陈思琪,王雷刚,黄瑶 - 《《基于杯突试验的镀锌板冲压成形失效分析》》
- 7Paint film flexibility bending test, which of these 5 instruments is more suitable?
- 8Cupping Testing Machine Test Coating Cupping Test
- 9Operation method and precautions of cupping instrument