Evaluation of film adhesion of different substrates by cross-cut tester
Overview
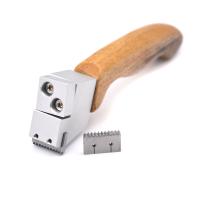
Adhesion is a key indicator of the bonding strength between the coating and the substrate, directly affecting the durability of the coating's functionality. The article "Evaluation of Paint Film Adhesion of Different Substrates with a Scratch Tester Instrument" uses the Hundred-Grid Knife (Scratch Tester) as its core tool, and in accordance with GB/T 9286 and ISO 2409 standards, systematically evaluates the paint film adhesion of common substrates such as metal, plastic, and wood. The instrument uses cutting templates with blade spacing of 1mm, 2mm, or 3mm, forming a grid through vertical cross-cutting. After tape peeling, the coating peeling area is observed to quantify adhesion grade. This article aims to provide standardized operating procedures and result interpretation methods to help inspectors quickly assess the adhesion performance of coatings on different substrates.
Principle of the test
The theoretical foundation of the grid method lies in simulating the mechanical stresses that coatings may encounter during actual use. The cutting action creates a cross-section on the coating surface, and the tensile force generated by the rapid peeling of the tape concentrates along the grid boundaries. If the bond strength between the coating and substrate is lower than this tensile strength, the coating will peel off at the mesh intersection or edge. The proportion of spalling area directly reflects the relative strength of adhesion: the more spalling there is, the poorer the adhesion.
The physical process of the experiment follows a simple mechanical relationship. Let the peeling force of the tape on the coating be F, the bond strength between the coating and substrate is σ, and the cutting mesh edge length is d, then the peel stress on a single grid is:
σPeel off = F / (d × Coating Thickness)
σ should be donePeel offPeeling occurs when the bond strength exceeds the coating-substrate interface. In actual evaluation, the value is not directly calculated; instead, the grading is determined by visually comparing standard images. This principle applies to all rigid or semi-rigid substrates, but cutting parameters need to be adjusted according to the surface characteristics of the substrate.
Sample preparation
Specimen preparation is the foundation of test reproducibility. Below is a detailed list of preparation requirements and parameters:
| Types of substrates | Reference requirements |
| Metals (steel, aluminum) | The surface is oil-free; after cleaning, it is dry. If necessary, lightly sand with 400-grit sandpaper to increase roughness |
| Plastics (ABS, PC, PA) | If the surface is free of release agents or contaminants, wipe with alcohol and let it air dry at room temperature |
| Wood (solid wood, medium-density fiberboard) | Moisture content is controlled between 8% and 12%, sanded to level, and wood chips are removed |
| Glass or ceramics | Thoroughly degreasing, with no fingerprints or residue allowed on the surface |
The choice of cutting parameters directly affects the number of grids and the comparability of the results. Based on coating thickness and substrate hardness, refer to the following cutting spacing:
| Coating thickness range | Recommended cutting spacing |
| ≤ 60 microns (hard substrate) | 1 mm (11 cuts× 11 cuts, total 100 slots) |
| 61 to 120 microns (hard substrate) | 2mm (6 cuts× 6 cuts, total 25 slots) |
| > 120 microns (soft or medium substrate) | 3mm (6 cuts× 6 cuts, total 25 slots) |
The recommended sample size is 10 cm × 15 cm. After the coating has fully cured, it should be left for at least 24 hours before cutting. Operating environment temperature is 23±2°C, relative humidity is 50±5%. The tool should be sharp and without notches; replace the blade after testing 5 samples.
Operating steps
Operational procedures follow standardized requirements to ensure that everyone receives comparable results every time. The specific steps are as follows:
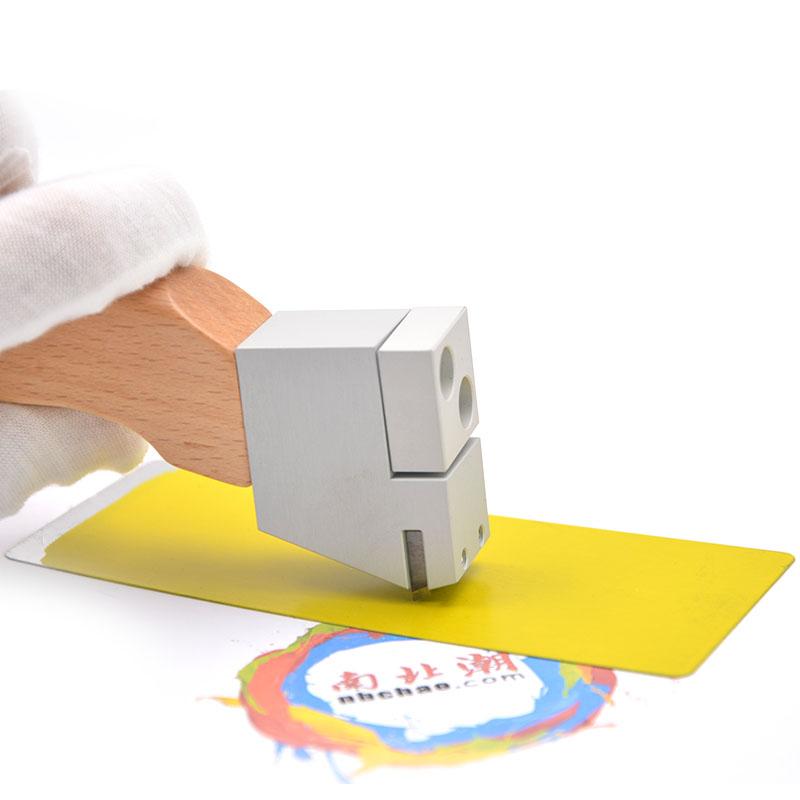
1. Place the specimen horizontally and use a grid cutter to cut at a uniform speed in one direction, keeping the blade tip at about a 90-degree angle to the substrate surface. The cutting depth must penetrate the coating and touch the substrate, with a cutting length of about 2 centimeters.
2. Repeat the cutting and form a mesh perpendicular to the direction of the first cut. Use a soft brush to gently sweep along the diagonal direction of the grid to remove any loose coating debris.
3. Press a standard pressure-sensitive tape with a width of 25 mm (adhesive strength not less than 4 N/25 mm) onto the mesh, then roll back and forth with a fingertip or rubber roller to ensure the tape fits tightly against the coating. The tape length is about 7.5 cm.
4. After waiting 5 minutes, grab the free end of the tape and quickly pull it off at an angle close to 60 degrees within 1 second.
5. Use a magnifying glass of no less than 10x to observe the mesh area and record the peel area.
Adhesion levels are classified according to GB/T 9286 from 0 to 5. The specific criteria are as follows:
| Level | Description of the stripping situation |
| 0 | The cutting edges are completely smooth, with no mesh detachment |
| 1 | Slight spalling at mesh intersections, with spalling area less than 5% |
| 2 | Intermittent spalling along the cutting edge, covering 5% to 15% of the area |
| 3 | Large areas of mesh shedding, covering 15% to 35% of the area |
| 4 | Most of the grid is detached, covering 35% to 65% of the area. |
| 5 | More than 65% of the peeling area can even peel off the entire layer |
Each sample tests at least three different regions, with the lowest grade used as the final result. If the differences among three regions exceed one grade, additional test points should be added and the average value reported. Data recording must retain the original photographs or microscope images.
Typical manifestations of different types of substrates
Based on extensive measured data, the adhesion strength of different substrates shows significant differences. After light grinding, aluminum panels typically reach grade 0 or 1 adhesion, with a peel area of almost zero; Untreated polypropylene (PP) plastic boards have low surface energy, with adhesion levels often between 3 and 4, causing the coating in the mesh to peel off in patches. Due to the moisture absorption of the wood surface and the direction of the wood grain, the grid along the grain direction may be easier to peel off, with grades between 1 and 2. If the glass substrate is not specially coupling, the adhesion is usually only level 2 to 3, and linear detachment appears at the mesh edges.
It is worth noting that the results of plastic substrates heavily depend on internal stresses or migration of low molecular weight generated during injection molding. It is recommended to use non-destructive methods (such as contact angle measurement) before testing to confirm whether the surface of the substrate meets the coating application requirements.
Common factors affecting results and corrections
Inspectors often encounter fluctuation in results, and the following factors require special attention:
First, insufficient cutting depth. If the blade does not fully penetrate the coating, tearing occurs during peeling rather than interface debonding, resulting in higher grades. The correction method is to check the knife marks after each cut, deepen the cut or replace the blade sharper if necessary.
Second, the type of tape. The adhesive strength of tapes from different manufacturers may vary by more than 10%, so standard tape should be used, with the grade and batch indicated in the report.
Third, environmental humidity. At high humidity, the coating may absorb moisture and soften, causing the coating to break inside when the tape peels off rather than stripping off from the substrate surface. In such cases, it is recommended to retest in a dry environment.
Fourth, coating aging. Testing should be conducted 24 to 72 hours after coating curing to avoid incomplete initial curing or long-term degradation.
For the phenomenon of high plastic substrate testing grades, the following comparison table can be used to assess whether pretreatment is needed:
| Surface condition of the substrate | Recommended pretreatment methods |
| Low surface energy (such as PP, POM) | Flame treatment, corona treatment, or plasma cleaning |
| There is a release agent residue | Solvent wiping + mechanical sanding |
| Water-soluble primer coating | Test after thorough drying |
The advantages of the grid tester method are its simple operation, low cost, and intuitive results, making it suitable for rapid on-site quality monitoring. For coatings of moderate thickness (20 to 200 microns), it is the most common evaluation method. The method is also suitable for flexible substrates (such as films), but requires a wider cutting spacing (3 mm) and supports with sponge backing.
However, this method has inherent limitations. It is not sensitive to systems with high cohesive strength and poor adhesion (such as certain fluorocarbon coatings), because the tape's tensile strength may not be sufficient to trigger peeling. In addition, substrates with rough textures (such as sandblasted steel plates) can cause irregular blade damage during cutting, leading to mesh deformation. In such cases, the pull-apart method (e.g., GB/T 5210) should be used for supplementary evaluation. For coatings with elastic modulus close to or lower than the adhesive strength of the tape (such as rubber-based anti-rust paint), it is recommended to use an adhesion tester (pull-out method) for verification.
Data recording
The test report should include the following to ensure traceability: sample number, substrate material and surface treatment method, coating system and thickness, test environment temperature and humidity, grid gauge specifications (blade spacing and number of blades), tape brand and batch, grade and average for each zone, and adhesion grade distribution map (optional). If the defect is determined to be grade 2 or higher, attaching microscopic images helps with defect analysis.
Case recording format reference: Using a 0.5mm thick aluminum plate as the substrate, spraying polyester powder coating, curing the film to be 80 microns thick, cutting with a 2mm tool pitch, three test areas rated as Grade 1, Grade 1, and Grade 2, with the final report as Grade 2. Two inspectors perform the procedure separately, with consistent results.
This method relies heavily on the operator's visual judgment, especially when the peeling boundary is blurry (such as cohesive fracture of the coating and interface detachment coexisting), and the level given by different personnel may differ by one level. The industry is experimenting with introducing digital image analysis systems to improve objectivity by automatically calculating the area of spallion. Additionally, the latest draft standard (such as the revised version of ISO 2409) recommends applying a 500-gram weight to pressure the tape at a constant rate to regulate the bonding pressure. For ultra-thin coatings (<15 microns), the grid method is almost unsuitable; in such cases, bending methods (such as tapered axis bending test) or scratch hardness testing should be prioritized.
In the future, online inspection devices combining acoustic emission or resistance induction principles may enable real-time, non-destructive monitoring of coating adhesion, but at present, scratch testers remain the most popular entry-level method.
Conclusion
The scratch tester provides a reliable and reproducible technical solution for evaluating the adhesion of paint films on different substrates. Through standardized operations and precise criteria, inspectors can quickly distinguish between qualified and unqualified coatings. Metal substrates can achieve high-grade adhesion with appropriate treatment; Plastic and wood require additional surface adjustments. This method is suitable for most rigid and semi-rigid substrates, but when dealing with highly elastic or ultra-thin coatings, it should be used in conjunction with other methods. It is recommended that laboratories regularly participate in proficiency testing and provide internal training for inspectors on visual discrimination to improve consistency in results.
References
GB/T 9286-2021 Colored Paint and Varnish - Grid Test
ISO 2409:2021 Paints and varnishes — Cross-cut test
ASTM D3359-23 Standard Test Methods for Rating Adhesion by Tape Test
Chen Xiaodong. Comparison of Adhesion Testing Methods for Plastic Surface Coatings [J]. Modern Coatings and Coatings, 2020, 23(4): 12-15.
Liu Qiang. Study on the Influence of Environmental Factors on Metal Coating Grid Test Results [D]. Chemical Equipment Technology, 2019, 40(6): 22-25.